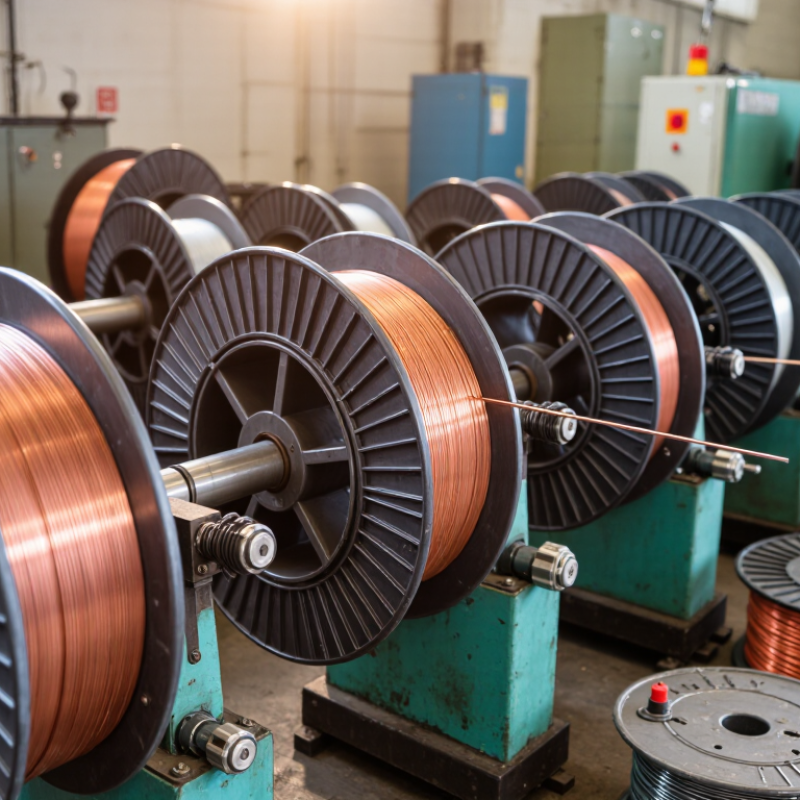
| 1 | Prepare the Empty Spool | The empty spool is mounted on the winding shaft and secured so that it rotates concentrically without excessive runout. | Winding shaft, chuck, collet, spool supports, locking mechanism | Spool core diameter: commonly about 50–500 mm, depending on the application. | The spool is centered, firmly clamped, and suitable for the wire size and finished coil weight. |
| 2 | Load and Align the Wire | The wire is fed from a payoff reel or supply container through the prescribed path toward the spool. | Payoff reel, guide rollers, ceramic or polymer guides, alignment sensors | Wire diameter: may range from fine wire below 0.1 mm to several millimetres in general winding applications. | The wire path is straight, unobstructed, and free from sharp contact points that could damage insulation or the conductor. |
| 3 | Set the Winding Direction | The control system selects clockwise or counterclockwise rotation according to the required coil orientation and lead position. | Drive motor, motor controller, programmable control system | Rotation direction: selected before starting; direction changes are normally made only when the machine is stopped or under controlled conditions. | The first wire lead is positioned at the specified starting location on the spool. |
| 4 | Apply Initial Tension | A controlled pulling force removes slack and keeps the wire seated against the spool without overstressing it. | Tensioner, dancer arm, load cell, magnetic or mechanical brake | Tension setting: selected according to conductor size, insulation type, tensile strength, and allowable elongation. | The wire remains stable during acceleration and does not visibly stretch, kink, buckle, or slip. |
| 5 | Start Spool Rotation | The winding shaft accelerates smoothly to the programmed speed while the controller monitors tension and position. | Electric motor, drive controller, encoder, emergency-stop circuit | Speed control: commonly adjusted from low-speed positioning to several hundred revolutions per minute; the safe limit depends on spool diameter, wire mass, and machine design. | Acceleration is smooth, with no sudden tension spike, wire whip, or spool movement. |
| 6 | Traverse the Wire Guide | A guide moves laterally across the spool face so each turn is placed beside the previous turn rather than randomly piling up. | Traverse carriage, lead screw, linear actuator, guide nozzle, position sensor | Traverse pitch: typically set close to the effective wire diameter for orderly adjacent winding; special patterns may use a different pitch. | The wire forms a uniform layer with consistent spacing and limited crossover. |
| 7 | Build Each Layer | When the guide reaches one flange, it reverses direction or follows the programmed pattern to create the next layer. | Traverse controller, limit sensors, spool flanges, position feedback system | Layer count: determined by the usable spool width, wire diameter, and required wire length or coil height. | Layers remain within the spool flanges and maintain an even, compact profile. |
| 8 | Measure Wire Length | The machine estimates or measures the amount of wire wound by using encoder feedback, a measuring wheel, or both. | Rotary encoder, measuring wheel, length counter, control software | Length calculation: based on measured feed movement or spool rotation combined with the effective winding diameter. | The target length is reached without relying solely on visual estimation. |
| 9 | Control Speed and Tension Continuously | As the coil diameter increases, the controller adjusts rotational speed and braking so the linear wire speed and tension remain within the selected limits. | Feedback controller, tension sensor, encoder, motor drive, brake | Control objective: stable tension and consistent deposition throughout the changing coil diameter. | The finished coil has consistent density, minimal loose loops, and no crushed or damaged insulation. |
| 10 | Stop at the Target | The machine decelerates when the programmed length, layer count, diameter, or weight is reached. | Controller, length sensor, diameter sensor, motor brake | Stop condition: may be length-based, diameter-based, layer-based, weight-based, or a combination of these. | The wire end is accessible and the coil remains secure without unraveling. |
| 11 | Secure and Cut the Wire | The wire is held against the spool or secured with tape, a clip, a tie, or a designated terminal before being cut. | Wire clamp, cutter, end-holder, labeling or marking device | Cutting method: selected according to wire material, diameter, insulation, and required end condition. | The cut end is clean, identified if necessary, and protected from unwinding or conductor damage. |
| 12 | Inspect and Remove the Finished Coil | The operator checks the winding appearance and removes the completed spool from the shaft for packaging or the next production operation. | Operator inspection tools, diameter gauge, weighing scale, spool-release mechanism | Inspection points: coil width, outer diameter, wire length, tension uniformity, end security, and visible surface damage. | The spool is ready for storage, transport, assembly, electrical testing, or further processing. |


 08045479132
 Send Inquiry

 Send Inquiry
 Send SMS