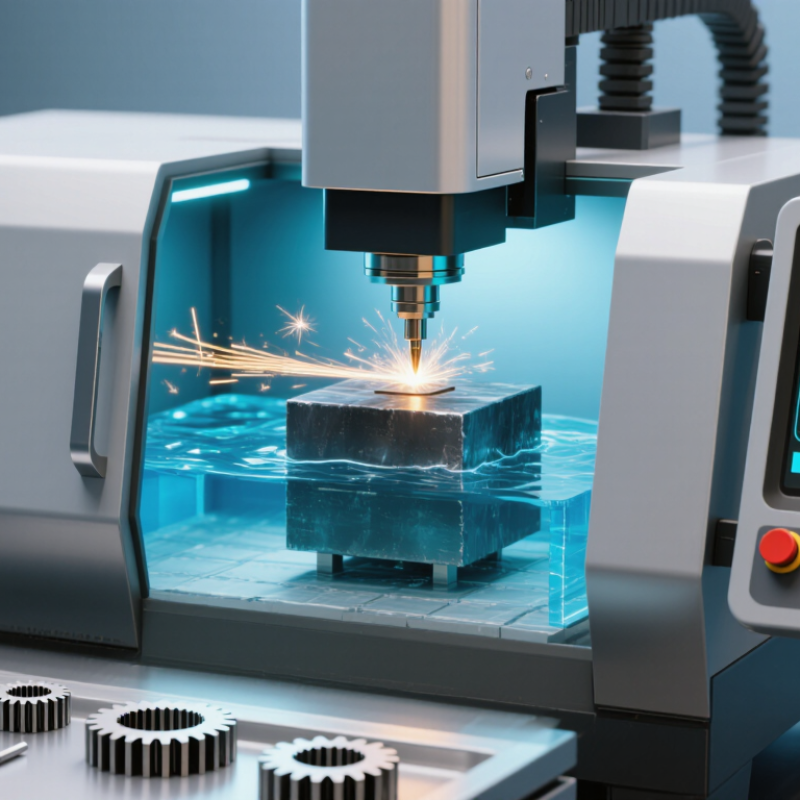
| Precision Dies | Tool steel, hardened steel, carbide, and conductive composite materials | Cuts hardened materials without applying conventional cutting forces, reducing the need for post-hardening machining | Punches, die openings, stripper plates, narrow slots, and fine blanking profiles | Approximately ±0.0025–0.010 mm under controlled conditions | Approximately Ra 0.2–1.6 µm, depending on cutting passes and process settings | Workpiece must be electrically conductive; wire diameter, flushing, thermal stability, and multiple skim cuts affect results |
| Mold Components | Hardened tool steel, stainless steel, conductive mold alloys, and graphite electrodes | Produces accurate internal profiles and sharp details after heat treatment, with minimal mechanical distortion | Cavity inserts, core components, ejector plates, slides, vent slots, and intricate contours | Approximately ±0.005–0.015 mm for many production applications | Approximately Ra 0.4–1.6 µm; finer finishes generally require additional skim cuts | Large or thick mold components require stable dielectric flushing and careful control of workpiece alignment |
| Conductive Carbide | Electrical-discharge-machinable cemented carbide and other electrically conductive hard materials | Machines extreme hardness without direct contact between the cutting wire and the workpiece | Wear inserts, carbide punches, forming tools, precision nozzles, and small slots | Approximately ±0.005–0.015 mm, subject to carbide grade, thickness, and machine condition | Approximately Ra 0.3–1.6 µm with suitable flushing and finishing passes | Electrical conductivity and binder composition influence cutting stability; brittle edges require controlled energy and flushing |
| Complex Tapered Profiles | Tool steel, hardened steel, carbide, titanium alloys, and other conductive metals | Independent upper and lower wire-guide movement enables programmed taper and changing-profile cuts | Tapered punches, turbine features, angled cores, sloped inserts, and 3D-contoured parts | Approximately ±0.010–0.030 mm on many tapered features, depending on height and angle | Approximately Ra 0.4–1.6 µm, with geometry and flushing affecting the final surface | Maximum taper angle, workpiece height, wire-guide travel, and collision clearance are machine-specific |
| Micro-Features and Fine Slots | Hardened steels, stainless steels, nickel alloys, and conductive carbide | Small wire diameters and non-contact cutting allow narrow slots, small radii, and delicate profiles | Fine apertures, miniature punches, narrow channels, and precision indexing features | Approximately ±0.005–0.020 mm, depending on feature size and material thickness | Approximately Ra 0.3–1.6 µm with optimized pulse parameters and finishing passes | Very small features are sensitive to wire deflection, debris removal, thermal conditions, and programming quality |
| Thick Precision Parts | Hardened tool steels, stainless steels, nickel-based alloys, and conductive superalloys | Can cut through substantial material thicknesses while maintaining a narrow kerf and avoiding tool wear from mechanical contact | Large die plates, thick inserts, precision gears, and complex through-features | Approximately ±0.010–0.030 mm, with accuracy influenced strongly by height and flushing | Approximately Ra 0.6–2.0 µm, depending on thickness and the number of finishing passes | Cutting speed and straightness may decline as thickness increases; adequate flushing and workholding are essential |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS