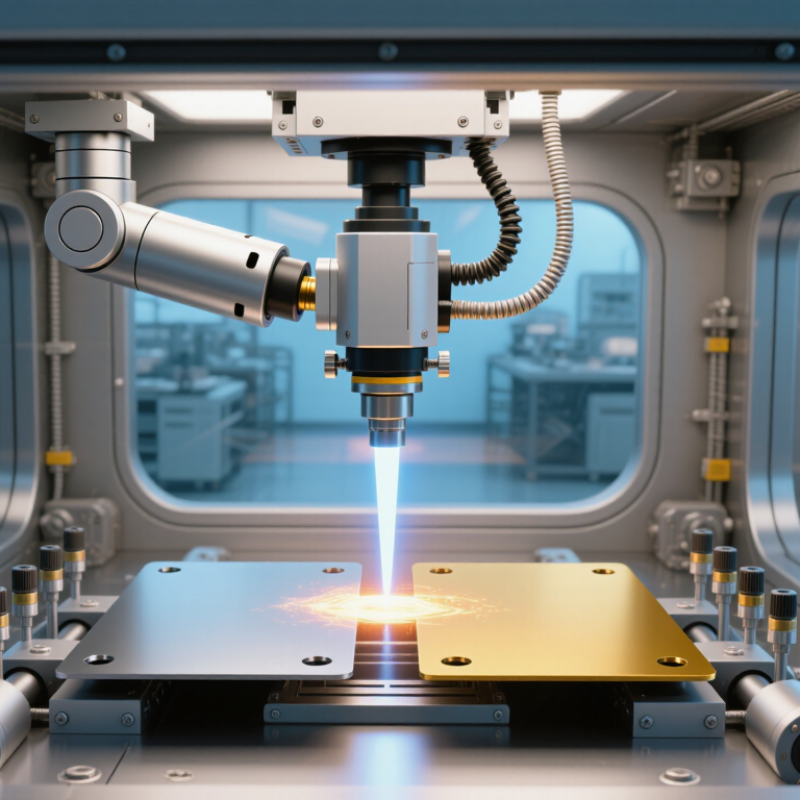
| Process Principle | Vacuum welding method | Solid-state joining under high vacuum | Joins clean, closely fitted surfaces without melting the parent materials. | Common mechanisms include diffusion bonding, hot pressing, and electron beam welding. |
| Vacuum Environment | Working pressure | Approximately 10−2 to 10−6 mbar, depending on the process | Reduces oxidation, contamination, and gas-related defects during heating or beam welding. | Required pressure depends on joint design, material, temperature, and equipment type. |
| Vacuum Equipment | Vacuum chamber | Sealed metal chamber with water-cooled or thermally protected walls | Contains the workpiece, tooling, heat source, and controlled atmosphere. | Chamber size must accommodate the component, fixtures, thermal expansion, and line-of-sight requirements. |
| Vacuum Equipment | Vacuum pumping system | Roughing pump plus high-vacuum pump | Removes air and vapor from the chamber before and during welding. | Rotary-vane, dry-scroll, turbomolecular, diffusion, or cryogenic pumps may be selected according to cleanliness and pressure needs. |
| Vacuum Equipment | Pressure measurement | Rough-vacuum and high-vacuum gauges | Monitors pump-down performance and maintains the required operating pressure. | Gauge readings should be interpreted according to gas type, temperature, and gauge operating range. |
| Vacuum Equipment | Heating system | Resistance, induction, radiant, or electron-beam heating | Raises the joint area to the required bonding or welding temperature. | Heating must be uniform enough to limit distortion and prevent excessive grain growth. |
| Vacuum Equipment | Temperature capability | Commonly about 600–1,200 °C for diffusion bonding; higher ranges are possible | Provides the thermal energy needed for atomic diffusion or localized fusion. | The maximum temperature is limited by the base materials, fixtures, chamber design, and joining method. |
| Vacuum Equipment | Force application system | Hydraulic, pneumatic, mechanical, or dead-weight loading | Maintains intimate contact between mating surfaces during diffusion bonding or hot pressing. | Pressure should be applied evenly to avoid gaps, distortion, or non-uniform bonding. |
| Vacuum Equipment | Process control and sensors | Pressure, temperature, displacement, current, and force monitoring | Records and controls the welding cycle for repeatable results. | Data logging helps verify heating rate, holding time, cooling rate, and vacuum stability. |
| Joint Preparation | Surface cleanliness | Degreased, oxide-free, and particle-free surfaces | Allows direct contact between the surfaces to be joined. | Oil, fingerprints, oxides, moisture, and machining residue can reduce bond strength and increase outgassing. |
| Joint Preparation | Surface roughness | Typically controlled to approximately Ra 0.4–3.2 µm, depending on the application | Improves real contact area while allowing practical machining and cleaning. | Lower roughness generally reduces voids, but excessive polishing may affect surface activation and cost. |
| Base Materials | Stainless steels | Austenitic and precipitation-hardening grades | Used for vacuum vessels, tooling, medical components, and corrosion-resistant assemblies. | Oxide removal and control of chromium-rich surface films are important before bonding. |
| Base Materials | Titanium and titanium alloys | Commonly joined in aerospace, chemical, and medical applications | Provide high specific strength and corrosion resistance. | Strong affinity for oxygen and nitrogen makes vacuum quality and surface preparation especially important. |
| Base Materials | Nickel-based alloys | High-temperature and corrosion-resistant alloys | Used in hot-section, chemical-processing, and high-performance engineering components. | Bonding temperature and time must be controlled to limit undesirable microstructural changes. |
| Base Materials | Aluminum and aluminum alloys | Lightweight alloys with high thermal conductivity | Used where low mass and good heat transfer are required. | Persistent aluminum oxide makes cleaning, activation, or an appropriate interlayer important. |
| Base Materials | Copper and copper alloys | High-conductivity materials for thermal and electrical components | Transfer heat or electrical current efficiently in compact assemblies. | High thermal conductivity can require controlled heating rates and sufficient dwell time. |
| Base Materials | Ceramics and refractory materials | Alumina, zirconia, silicon carbide, and related materials | Provide high-temperature stability, wear resistance, or electrical insulation. | Differences in thermal expansion between ceramics and metals can create residual stress. |
| Interlayers | Metal foil or coating | Often tens to hundreds of micrometres thick | Improves contact, promotes diffusion, or helps join dissimilar materials. | Interlayer composition and thickness influence reaction phases, joint strength, and operating temperature. |
| Consumables | Cleaning agents and preparation tools | Solvent cleaners, lint-free wipes, abrasive finishing media, and controlled handling tools | Removes oils, particles, and weak surface films before loading the chamber. | Cleaning materials must leave minimal residue and should be compatible with vacuum service. |
| Process Cycle | Typical sequence | Load → evacuate → heat → apply force or beam → hold → cool → vent | Creates a controlled thermal, mechanical, and vacuum environment for joining. | Cooling under vacuum is often used to reduce oxidation and thermal shock. |
| Quality Control | Common inspection methods | Visual inspection, dimensional checks, leak testing, microscopy, and non-destructive testing | Confirms joint integrity, alignment, cleanliness, and the absence of unacceptable defects. | Ultrasonic, radiographic, dye-penetrant, or helium leak testing may be selected for the application. |
| Advantages | Primary benefits | Low oxidation, minimal filler use, clean joints, and suitability for dissimilar materials | Supports high-integrity assemblies with limited post-weld finishing. | Results depend strongly on surface preparation, fit-up, vacuum quality, temperature, pressure, and cycle time. |
| Limitations | Key constraints | High equipment cost, limited chamber size, long cycle times, and strict cleanliness requirements | Defines when vacuum welding is technically and economically appropriate. | Large or highly outgassing components may require special fixtures, longer pump-down times, or alternative joining methods. |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS