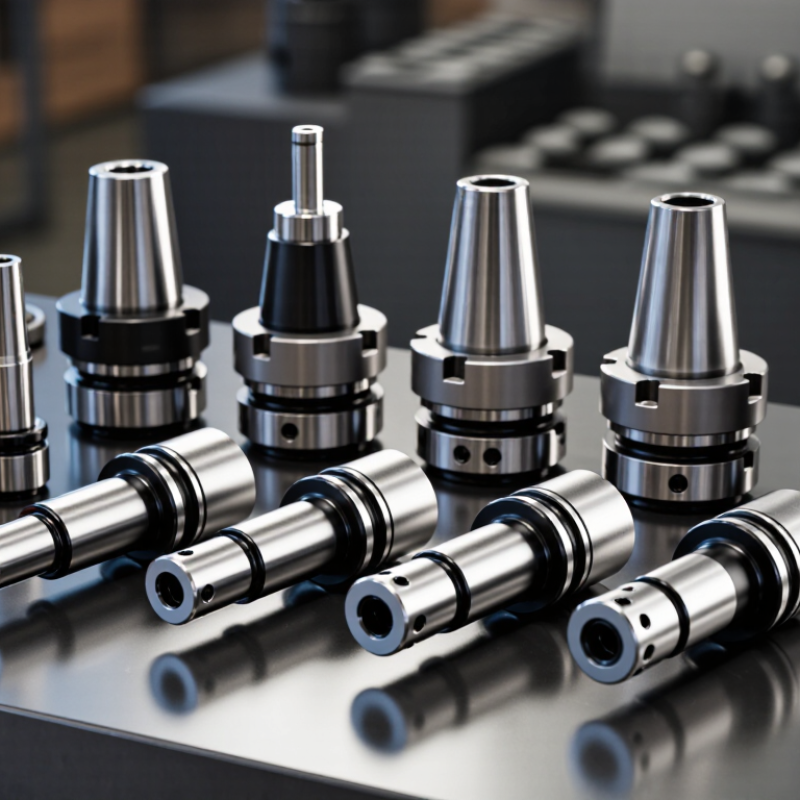
| 1 | HSK-A63 Heavy-Duty Shrink Fit Holder
Short gauge length, thick wall | 6–25 mm
0.236–0.984 in | ≤3 µm
at 3×D | G2.5 at 25,000 rpm | Very High
★★★★★ | High-speed roughing, hard milling, die and mold work | Through-tool coolant; sealed design commonly available | Medium–High | Excellent stiffness, but less suitable for very small cutters |
| 2 | BT40 Dual-Contact Shrink Fit Holder
Balanced flange and taper contact | 3–20 mm
0.118–0.787 in | ≤3 µm
at 3×D | G2.5 at 20,000 rpm | Very High
★★★★★ | General production milling, roughing, and finishing | Through-tool coolant; peripheral coolant options | High | Strong all-round choice, but requires a dual-contact spindle interface |
| 3 | HSK-A100 High-Rigidity Shrink Fit Holder
Large taper with reinforced body | 10–32 mm
0.394–1.260 in | ≤4 µm
at 3×D | G2.5 at 18,000 rpm | Very High
★★★★★ | Large-diameter tools, heavy stock removal, aerospace structures | Through-tool coolant; high-pressure configurations available | Medium | Maximum rigidity with greater mass and a larger spindle requirement |
| 4 | HSK-E50 High-Speed Shrink Fit Holder
Compact, symmetrical body | 3–16 mm
0.118–0.630 in | ≤3 µm
at 3×D | G2.5 at 30,000 rpm | High
★★★★☆ | High-speed finishing, small-diameter milling, graphite machining | Through-tool coolant; sealed nose designs common | High | Excellent speed capability, but less rigid than larger taper systems |
| 5 | CAT40 Slim Shrink Fit Holder
Reduced-nose design for accessibility | 3–16 mm
0.118–0.630 in | ≤3 µm
at 3×D | G2.5 at 20,000 rpm | High
★★★★☆ | Deep cavities, five-axis work, finishing near walls | Through-tool coolant; external coolant on compact models | High | Good access and low interference, with reduced wall thickness |
| 6 | BT50 Heavy-Duty Shrink Fit Holder
Large flange and high load capacity | 12–32 mm
0.472–1.260 in | ≤4 µm
at 3×D | G2.5 at 15,000 rpm | Very High
★★★★★ | Heavy roughing, large cutters, high-torque machining centers | Through-tool coolant; high-pressure sealing options | Medium | Very rigid, but not optimized for high spindle speeds or tiny tools |
| 7 | HSK-F63 Slim Shrink Fit Holder
Long-reach, low-interference profile | 3–20 mm
0.118–0.787 in | ≤3 µm
at 3×D | G2.5 at 25,000 rpm | Medium–High
★★★★☆ | Five-axis machining, deep pockets, complex mold components | Through-tool coolant; external coolant commonly supported | High | Excellent accessibility, with lower rigidity than short heavy-duty holders |
| 8 | SK40 Standard Shrink Fit Holder
General-purpose steep-taper format | 3–20 mm
0.118–0.787 in | ≤5 µm
at 3×D | G2.5 at 15,000 rpm | High
★★★★☆ | Routine production milling and general toolroom work | Through-tool coolant; depends on retention-knob and holder design | High | Broad machine compatibility, but typically lower speed capability |
| 9 | HSK-E40 Precision Shrink Fit Holder
Small taper for miniature tooling | 1–12 mm
0.039–0.472 in | ≤3 µm
at 3×D | G2.5 at 35,000 rpm | Medium
★★★☆☆ | Micro-milling, electronics, medical parts, and graphite electrodes | Through-tool coolant; air blast is common for micro-tools | Medium | Very accurate at high speed, but limited to smaller tool diameters |
| 10 | Compact Modular Shrink Fit Holder
Short body for restricted work envelopes | 3–16 mm
0.118–0.630 in | ≤5 µm
at 3×D | G2.5 at 20,000 rpm | Medium
★★★☆☆ | Compact machining centers, short-reach work, and mixed production | Through-tool coolant; configuration dependent | High | Flexible and compact, but modular joints can reduce overall rigidity |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS