| Quality Management | ISO 9001 | A documented quality management system covering design, purchasing, machining, plating, inspection, nonconformance control, and corrective actions. | Valid certificate, certification scope, issuing body, expiry date, and recent audit status. | Helps demonstrate repeatable production controls, but does not by itself prove valve or coating performance. |
| Valve Design and Pressure Rating | ASME B16.34 | Pressure–temperature rating, materials, wall thickness, end connections, bolting, marking, and design limitations appropriate to the selected valve type. | Approved drawings, pressure class or PN designation, material specifications, and design calculation records where applicable. | Confirms that the valve body and pressure-retaining parts are designed for the intended service conditions. |
| Pipeline Valve Qualification | API 6D / ISO 14313 | Applicability to pipeline gate, ball, plug, and check valves; design, manufacturing, testing, documentation, and marking requirements. | Product certificate, type designation, test records, and confirmation that the certificate covers the supplied valve configuration. | Important for oil, gas, and pipeline projects where a recognized pipeline valve standard is specified. |
| Pressure and Leakage Testing | API 598 or ISO 5208 | Shell test, seat test, test pressure, test duration, leakage rate, test medium, and acceptance level specified for the valve design. | Signed inspection and test report showing valve identification, applied pressure, duration, leakage result, and inspector approval. | Chrome plating cannot compensate for poor seat geometry, damaged sealing surfaces, or inadequate pressure testing. |
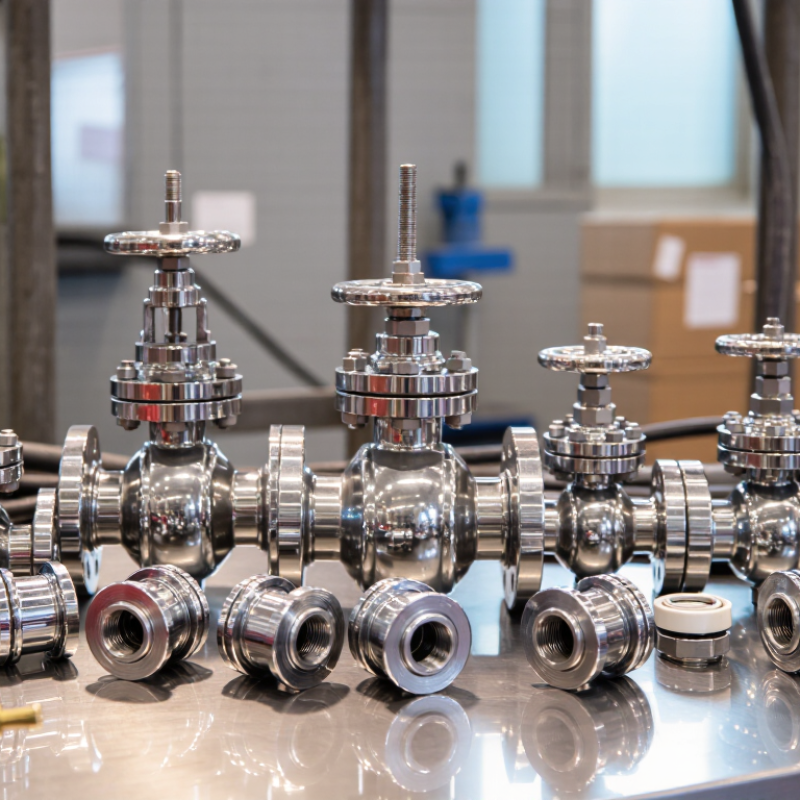
| Chrome Coating System | ISO 1456 | Type of electrodeposited nickel and chromium coating, substrate preparation, coating designation, service environment, and specified coating thickness. | Coating specification, plating process sheet, surface-preparation procedure, and coating designation stated on the purchase order or drawing. | Chrome appearance alone is not sufficient; the complete coating system and intended environment must be defined. |
| Coating Thickness Verification | ASTM B568 or ASTM B487 | Measured coating thickness at functional and representative locations, including edges, bores, sealing surfaces, and high-wear areas where accessible. | X-ray fluorescence report or metallographic cross-section report with instrument calibration and measurement locations. | Adequate and uniform thickness supports wear resistance and dimensional control; the required value must be agreed for each application. |
| Coating Adhesion and Surface Condition | Approved coating procedure; project-specific adhesion test | No blistering, peeling, flaking, exposed substrate, excessive roughness, visible cracks, or plating defects that could affect sealing or operation. | Visual inspection record, surface-finish readings where specified, adhesion test results, and nonconformance reports. | Poor adhesion can cause particles, corrosion sites, dimensional changes, and premature damage to seats or mating parts. |
| Corrosion Resistance | ASTM B117 or ISO 9227 | Whether neutral salt spray testing is required, the exposure duration, specimen preparation, and the agreed rating or failure criteria. | Laboratory test report identifying coating system, test duration, specimen condition, and evaluation method. | Salt spray results are comparative evidence and should not be treated as a direct prediction of every field environment. |
| Sour-Service Materials | NACE MR0175 / ISO 15156 | Material suitability for hydrogen sulfide-containing oil and gas environments, including hardness, metallurgy, heat treatment, and environmental limits. | Material certificates, hardness results, heat-treatment records, and a written compliance statement for the specified service. | Chrome plating does not automatically make a valve suitable for sour service; base materials and operating conditions remain critical. |
| Fugitive Emissions | ISO 15848-1 or ISO 15848-2 | Stem or shaft sealing performance, test medium, temperature, mechanical cycles, and leakage classification required by the project. | Type-test report or production test record identifying packing, seal arrangement, temperature, cycles, and measured leakage. | Relevant for chemical, petrochemical, and other facilities where valve emissions are regulated or tightly controlled. |
| Traceability and Documentation | EN 10204 inspection documents | Traceability from heat number and raw material through machining, heat treatment, plating, inspection, assembly, and final testing. | Material certificates, heat-treatment charts, plating records, dimensional inspection reports, pressure-test reports, and final data book. | Complete records make future maintenance, failure analysis, and regulatory review more reliable. |
| Dimensional Interchangeability | ASME B16.10; ASME B16.5 or ASME B16.47 where applicable | Face-to-face or end-to-end dimensions, flange dimensions, bolt-hole layout, pressure class, and compatibility with connected equipment. | Dimensioned drawings, inspection report, flange standard, and dimensional certificate for the supplied batch. | Correct dimensions reduce installation problems and prevent field modification that could damage the coating or pressure boundary. |
| International Marking and Identification | MSS SP-25; applicable product standard | Clear marking of size, pressure class or rating, material, flow direction where required, manufacturer trace code, and applicable conformity information. | Marking photographs, nameplate details, traceability procedure, and sample identification records. | Accurate identification supports receiving inspection, installation, maintenance, and replacement planning across international sites. |
| Production Capacity and Delivery Control | Contract-specific quality plan and inspection plan | Available machining and plating capacity, subcontractor control, batch size capability, lead-time assumptions, inspection resources, and contingency planning. | Manufacturing schedule, quality plan, inspection and test plan, capacity statement, and documented subcontractor controls. | A technically capable supplier must also deliver consistent batches within the required schedule and documentation format. |


 08045479132
 Send Inquiry

 Send Inquiry
 Send SMS