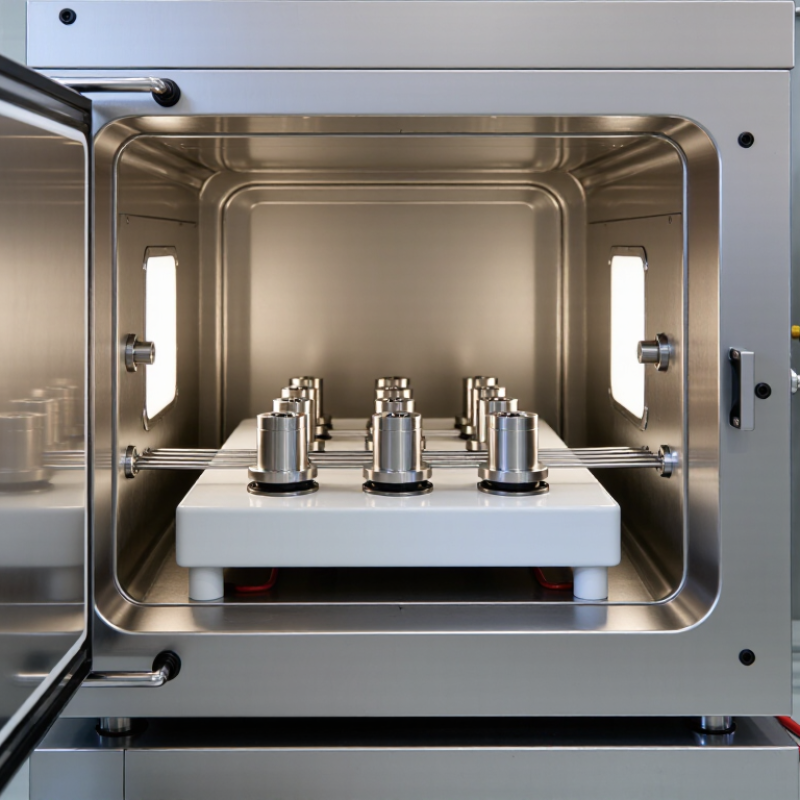
| Controlled cooling | After the brazing hold, cool the load according to the approved cycle. Cooling may use furnace radiation, controlled gas cooling, or another qualified method. The appropriate rate depends on the alloy, component geometry, joint design, and any required heat treatment. | Confirm that the cooling profile follows the approved procedure and that the parts are supported to limit distortion. Avoid rapid cooling unless it has been qualified for the materials and assembly. | Cooling curve, thermocouple readings, furnace-cycle identification, and any alarms or cycle deviations. |
| Temperature check before venting | Keep the chamber under vacuum or a specified protective atmosphere until the load reaches the procedure’s permitted venting temperature. The limit is process-specific; there is no single temperature suitable for every alloy or furnace. | Verify the indicated load or furnace temperature—not just the elapsed cooling time—before introducing gas or opening the chamber. | Temperature at venting, atmosphere or gas used, and the applicable procedure revision. |
| Chamber venting | When permitted by the cycle, restore the chamber to atmospheric pressure using the specified gas, commonly a clean inert gas such as argon or nitrogen where appropriate. | Check that the venting method matches the material and cleanliness requirements. Prevent exposure to air while parts are still hot if oxidation could affect the assembly. | Venting gas, chamber pressure status, and any atmosphere or cleanliness checks required by the process. |
| Unloading and handling | Remove the load only after the chamber is safe to open and the components are cool enough for the prescribed handling method. Use clean gloves or suitable handling tools when surface contamination is a concern. | Look for loose fixtures, shifted components, visible discoloration, damage, or signs of distortion. Handle the assembly carefully to avoid bending joints or contaminating clean surfaces. | Load identification, unloading time, operator, fixture condition, and any visible observations. |
| Visual and dimensional inspection | Inspect accessible joints and compare critical dimensions with the engineering drawing or inspection plan. Magnification may help reveal surface indications, but visual inspection cannot establish the condition of every hidden joint. | Check for incomplete filler-metal flow, excessive filler metal, cracks, visible voids, distortion, and blocked passages where applicable. Assess dimensions against specified tolerances. | Inspection results, measurement values, photographs when required, and any nonconformance reports. |
| Functional or nondestructive testing | Use tests selected for the assembly’s function and acceptance requirements. Examples include pressure or leak testing, radiographic examination, or other qualified nondestructive methods. | Apply the specified test method, test pressure or sensitivity, duration, and acceptance limits. These requirements must come from the drawing, customer specification, or approved quality plan. | Test method, equipment identification, calibrated instrument status, measured results, and pass/fail disposition. |
| Final release | Review the furnace-cycle record and inspection results before accepting the assembly for the next operation or shipment. | Confirm traceability, completion of required checks, and documented disposition of any deviations. Do not treat a visually sound joint as proof of leak-tightness or internal integrity. | Final inspection approval, material and load traceability, cycle record, and signed release status. |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS