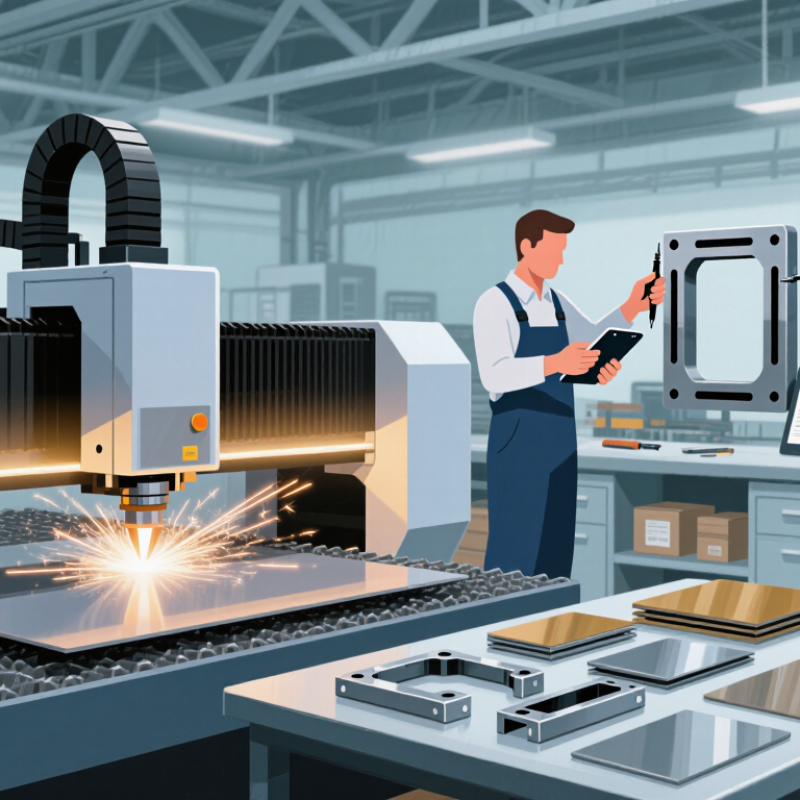
| ISO 9013:2017 classification | Confirm that the supplier identifies the applicable quality range for the specified thermal cut and part requirements. ISO 9013 covers geometrical product specifications and quality tolerances for thermal cuts. | Which ISO 9013:2017 quality range can you achieve for this material, thickness, and cut geometry? | A quotation or technical specification naming the standard edition, agreed quality range, material, and thickness. |
| Class 1 | Highest quality range in the Class 1–5 scale. Consider it when cut-face geometry and surface quality are especially demanding. | Can you demonstrate Class 1 performance on a representative part and production material? | Inspection results from a comparable job, with the measurement method and test conditions stated. |
| Class 2 | High quality range that may suit parts with tighter cut-quality needs than general-purpose work. | Which drawing features or downstream operations could affect the achievable range? | A sample-part report and agreement on the characteristics that will be inspected. |
| Class 3 | Intermediate quality range that may be appropriate for many functional parts, depending on the drawing and application. | Will the proposed cut quality meet our fit, assembly, and finishing requirements? | A first-article inspection plan tied to the drawing and agreed acceptance criteria. |
| Class 4 | Lower quality range than Classes 1–3. Check whether additional finishing or looser design requirements are acceptable. | Will the cut edge need grinding, deburring, or other post-processing? | A sample cut, finishing scope, and confirmation of which features are included in inspection. |
| Class 5 | Lowest quality range in the Class 1–5 scale. Confirm suitability carefully before specifying it for a functional edge or precision assembly. | Does this range meet the part’s functional requirements without unplanned rework? | A written acceptance agreement and representative sample reviewed against the drawing. |
| Cut-face geometry | Review the applicable ISO 9013 characteristics, including perpendicularity or angularity tolerance and the mean height of the profile, where relevant to the cut. | Which characteristics will you measure, and how will results be recorded? | Measured results with units, measurement locations, equipment or method, and material thickness identified. |
| Material and thickness | Quality results depend on the material, thickness, machine setup, and cutting conditions. Do not assume a result on one job applies to every job. | Is the quoted quality range confirmed for our exact material grade and thickness? | A process or capability statement for the specified material and thickness, plus a production sample when needed. |
| Edge condition and secondary work | Agree on requirements for burrs, dross, heat effects, edge finishing, and any cosmetic limits separately where they are important to the application. | What edge condition is included in the price, and what finishing is optional? | A sample part, written edge-condition criteria, and a clearly itemized finishing scope. |
| Inspection and acceptance | Make acceptance criteria measurable and consistent with the drawing, the selected ISO 9013 range, and the intended use of the part. | Can you provide first-article and ongoing inspection records for the agreed characteristics? | A documented inspection plan, sample report, and agreed process for handling nonconforming parts. |
| Procurement note: ISO 9013 quality ranges are not a substitute for specifying all part requirements. Agree on the applicable range and relevant characteristics for the actual material, thickness, geometry, and application; consult the standard for exact tolerances and measurement requirements. |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS