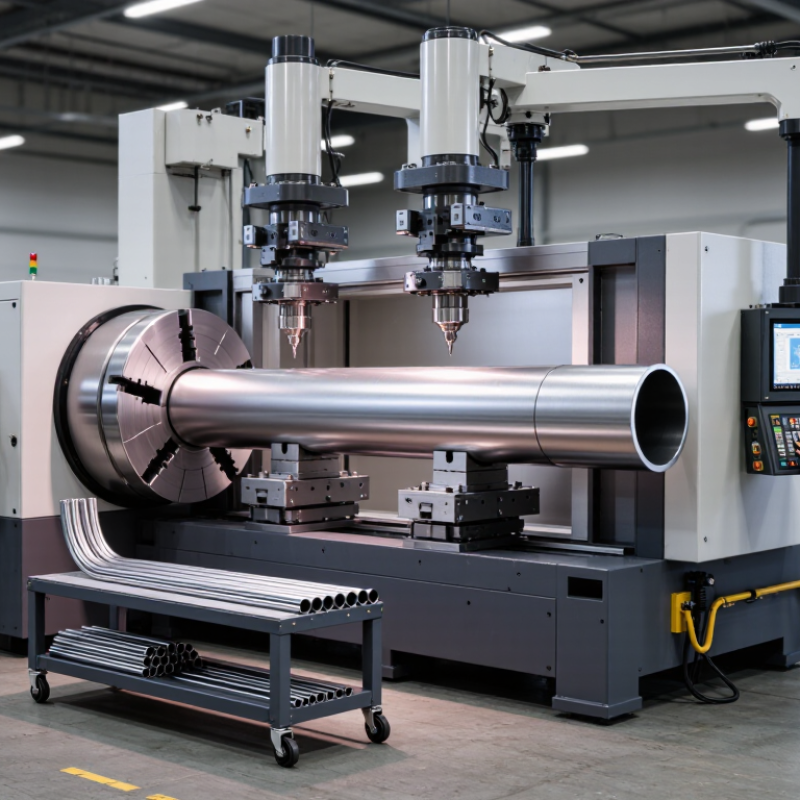
| Workpiece capacity | Tube or pipe outside diameter, wall thickness, length, and material grade. | The rated working range must cover the largest and smallest parts in the production mix—not just the nominal pipe size. | Swaging load depends on material strength, wall thickness, reduction, and tooling; diameter alone does not define capacity. | Submit representative part drawings and material details for a capacity review or sample run. |
| Reduction and finished geometry | Required end diameter, taper, transition length, concentricity, and dimensional tolerance. | Confirm the machine and die design can achieve the specified geometry, including any staged reduction or intermediate annealing requirements. | Excessive reduction in one operation can cause cracking, wrinkles, or out-of-tolerance parts. | Review process limits and inspect trial parts with appropriate gauges or measuring equipment. |
| Production rate | Required parts per hour, operating hours per shift, changeover frequency, and loading method. | Compare demonstrated cycle time, including loading, forming, inspection, and tool changes—not just the machine’s stroke rate. | A high forming speed does not guarantee the required output if handling or setup is the bottleneck. | Request a timed production trial using the intended part and operator workflow. |
| Controls and repeatability | Stroke or position adjustment, speed control, stored recipes, status indicators, and fault diagnostics. | Choose controls that let operators set and repeat validated process parameters with suitable access control and clear fault messages. | Repeatable settings help reduce setup variation, scrap, and dependence on individual operator experience. | Check a demonstration of recipe setup, parameter adjustment, alarm handling, and restart after a fault. |
| Tooling and changeover | Die and guide range, material compatibility, tool availability, changeover time, and setup method. | Confirm tooling is available for every required size and profile, with clear identification and a repeatable alignment procedure. | Correctly matched, maintained tooling supports surface quality, dimensional accuracy, and reliable feeding. | Obtain a tooling list, changeover instructions, maintenance guidance, and replacement lead-time details. |
| Safety features | Point-of-operation guarding, interlocked access, emergency stops, safe setup mode, and lockout provisions. | Verify safeguards suit the actual machine layout and intended tasks, including feeding, tool changes, cleaning, and maintenance. | Swaging equipment has moving and pinch-point hazards; safeguards must be assessed as part of the complete installation. | Review the risk assessment, safety documentation, guarding, and applicable local machinery requirements before operation. |
| Maintenance and support | Routine service intervals, wear parts, lubrication needs, documentation, and technician availability. | Favor a maintainable design with documented service tasks and accessible replacement parts. | Planned maintenance helps preserve accuracy and reduce unplanned downtime. | Review the maintenance schedule, spare-parts list, training options, and service response arrangements. |
| Installation requirements | Floor space, foundation or anchoring, electrical supply, compressed air if required, and noise level. | Match the machine’s documented utility and installation requirements to the available site conditions. | Insufficient utilities or space can delay commissioning and complicate safe operation and maintenance access. | Use the installation drawing and utility schedule to complete a site-readiness check before delivery. |


 08045479132
 Send Inquiry

 Send Inquiry
 Send SMS