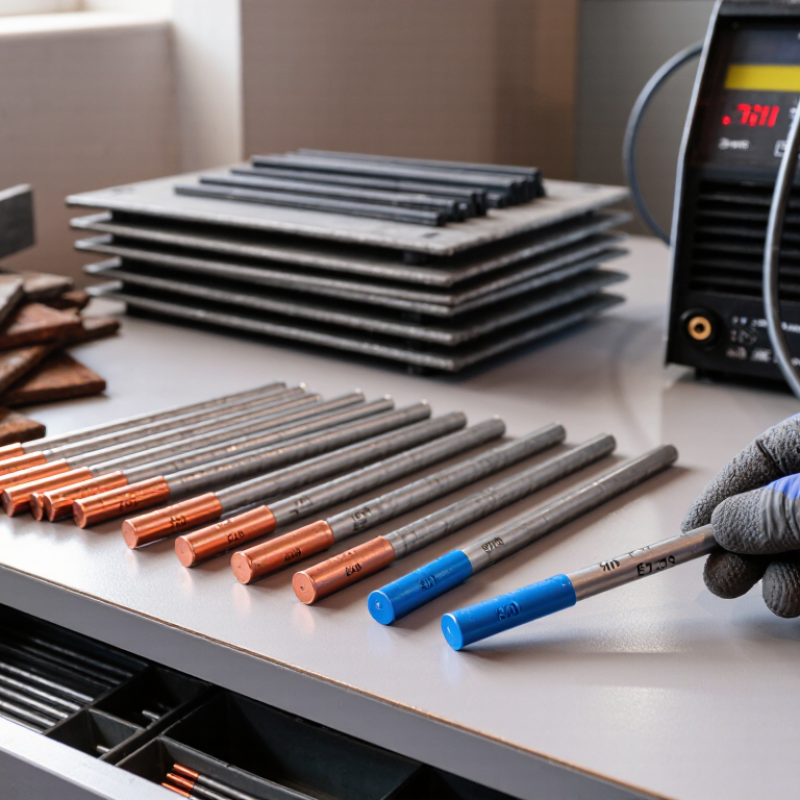
| General-purpose carbon steel; clean material; repair or fabrication | E6013 | Suitable for many positions and common joints, including fillets and butt joints; often chosen for lighter-gauge work and a smoother bead. | Commonly AC, DCEP, or DCEN; check the electrode package for the approved current range. | Has relatively moderate penetration and is often easier to use on small AC machines than some other electrodes. Use a suitable electrode diameter for the material thickness. |
| Carbon steel requiring deeper penetration, including open-root work | E6010 | All-position electrode commonly used for root passes and pipe work where deep penetration is needed. | Typically DCEP; generally not suitable for ordinary AC output. | Cellulosic coating produces a forceful arc and fast-freezing slag. Confirm that the power source and welding procedure support this electrode. |
| Carbon steel with an AC-only power source, or less-than-perfect surface conditions | E6011 | All-position use; can be used for many repair joints and root passes. | Commonly AC or DCEP. | Can tolerate some mill scale or light surface contamination better than low-hydrogen electrodes, but it does not replace proper cleaning. Not a substitute for determining the required weld quality. |
| Carbon steel requiring higher tensile strength or a low-hydrogen weld deposit | E7018 | All-position electrode commonly used for structural and general fabrication work. | Commonly AC or DCEP, depending on the specific classification and product. | Keep electrodes dry and follow the required storage and exposure limits. Moisture control is important where low-hydrogen welding is specified. |
| Carbon steel where a higher deposition rate is desired on flat or horizontal work | E7024 | Primarily designed for flat and horizontal fillet welding; not a general all-position choice. | Commonly AC or DC; verify the permitted polarity for the specific electrode. | Iron-powder coating supports a high deposition rate. Best suited to joints and positions that allow a larger, fast-filling bead. |
| Stainless steel similar to Type 304 | E308L-16 | Used for joining compatible 304/304L stainless steel; suitable joint preparation and position depend on the specific electrode and procedure. | Commonly AC or DCEP for the -16 coating type; confirm the product instructions. | The “L” indicates low carbon in the deposited weld metal. Match the filler classification to the stainless grade and service requirements. |
| Joining stainless steel to carbon steel or other dissimilar metals | E309L-16 | Often selected for dissimilar joints involving stainless and carbon steel; joint design and procedure remain important. | Commonly AC or DCEP for the -16 coating type; confirm the product instructions. | Do not select by base-metal appearance alone. Confirm compatibility with the actual alloys, dilution, and service conditions. |
| Stainless steel similar to Type 316 | E316L-16 | Used for compatible 316/316L stainless-steel joints; position capability depends on the electrode specification. | Commonly AC or DCEP for the -16 coating type; confirm the product instructions. | Typically chosen where the weld metal needs to be compatible with molybdenum-bearing 316 stainless. Check corrosion and service requirements before welding. |
| Thin material, limited access, or a small welding machine | Choose a suitable diameter and classification for the base metal; E6013 is one common option for light work. | Match the electrode diameter and bead size to the joint gap, material thickness, and welding position. | Stay within the machine’s output and the electrode’s stated amperage range. | A smaller diameter generally operates at lower current and can help control heat input, but fit-up, technique, and burn-through risk still matter. |
| Outdoor work or a drafty location | Select an electrode suitable for the metal and procedure; low-hydrogen electrodes may be specified for strength-critical work. | Consider wind exposure, joint access, and whether the work can be shielded. | Use the polarity and current range specified for the selected electrode. | Stick welding does not rely on an external shielding-gas envelope, but wind, moisture, and contamination can still affect weld quality. Protect the joint and keep electrodes dry as required. |
| Selection check: Identify the base-metal grade and thickness, joint type, welding position, required mechanical properties, power-source output, and permitted polarity. Follow the applicable welding procedure, electrode instructions, and code requirements; classification alone does not establish that an electrode is suitable for every job. |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS