| 1. Application Definition | Load and motion profile | Specify radial load, axial load, moment load, stroke, speed, duty cycle, and expected service life before requesting quotations. | Example: 2,000 N radial load; 500 N axial load; 100 mm stroke; 60 cycles/min; minimum L10 life of 10,000 km. | Preload, clearance, mounting orientation, lubrication type, and sealing arrangement can be matched to the application. | Review load calculations and verify operating conditions against the bearing load rating and manufacturer calculation sheet. | Request a technical quotation with assumptions, exclusions, service-life calculation, and validity period. |
| 2. Product Selection | Size and dimensional compatibility | Confirm shaft or table dimensions, mounting-hole pattern, overall height, effective stroke, and available installation space. | Example sample: 80 mm nominal rail length; 60 mm carriage length; 30 mm width; 12 mm height; 50 mm effective stroke. | Non-standard lengths, carriage configurations, mounting holes, end seals, and rail-to-carriage combinations may be requested. | Measure with calibrated vernier calipers, micrometers, height gauges, and a coordinate measuring machine where required. | Require a controlled drawing with revision number, tolerance table, material, heat-treatment condition, and inspection datum. |
| 3. Sample Approval | Sample quantity and traceability | Order at least three samples from the intended production route when repeatability and preload consistency are important. | Each sample should carry a lot number, production date, dimensional report, material certificate, and lubrication record. | Sample drawings and production drawings must use the same revision-controlled specifications before approval. | Check dimensions, smooth travel, abnormal noise, starting torque, preload, and visual condition against an approved sample report. | Define sample approval as a purchase milestone; mass production should not begin before written approval. |
| 4. Accuracy and Preload | Running accuracy and internal preload | Select an accuracy class and preload grade suitable for the machine stiffness, positioning accuracy, and operating speed. | Typical precision applications may require running parallelism in the tens of micrometres per metre and controlled preload variation. | Specify light, medium, or heavy preload only after checking friction, heat generation, rigidity, and drive capacity. | Use a force gauge or torque measurement system for preload and a dial indicator or laser measurement system for running accuracy. | The purchase order should state the accuracy class, preload grade, measurement direction, measuring speed, and acceptance limits. |
| 5. Materials and Manufacturing | Rail, roller, and retainer quality | Confirm bearing steel grade, hardness range, heat treatment, roller geometry, retainer material, and surface protection. | Typical bearing-steel components are through-hardened or case-hardened according to the design; the exact grade must be stated on the drawing or certificate. | Options may include corrosion-resistant steel, special coatings, high-temperature grease, or clean-environment materials. | Review mill certificates, hardness test records, surface-finish readings, and heat-treatment traceability. | Require change notification for material, heat treatment, production location, tooling, lubricant, or subcontracting changes. |
| 6. Lubrication and Environment | Operating environment | Define temperature, dust, moisture, vacuum, cleanroom class, corrosion exposure, and relubrication interval. | Example requirement: operating range of 10–40 °C, standard industrial atmosphere, protected from direct coolant and abrasive dust. | Grease type, filling quantity, seals, wipers, stainless components, and cleanroom cleaning can be customized when technically feasible. | Verify lubricant identification, fill quantity, seal contact, contamination level, and travel noise during a functional test. | Require safety data sheets and storage instructions; specify shelf-life, packaging humidity protection, and first-use date limits. |
| 7. Inspection Planning | Pre-shipment quality control | Use a written inspection plan covering critical dimensions, appearance, preload, smoothness, noise, packaging, and documentation. | Suggested sampling: 100% inspection for critical dimensions and function; statistical sampling for non-critical cosmetic items. | Agree on critical-to-quality characteristics, inspection equipment, sampling level, and nonconformance disposition before production. | Use calibrated equipment with valid certificates and retain inspection records linked to the shipment lot. | Payment balance may be linked to an accepted inspection report, subject to the agreed purchase contract. |
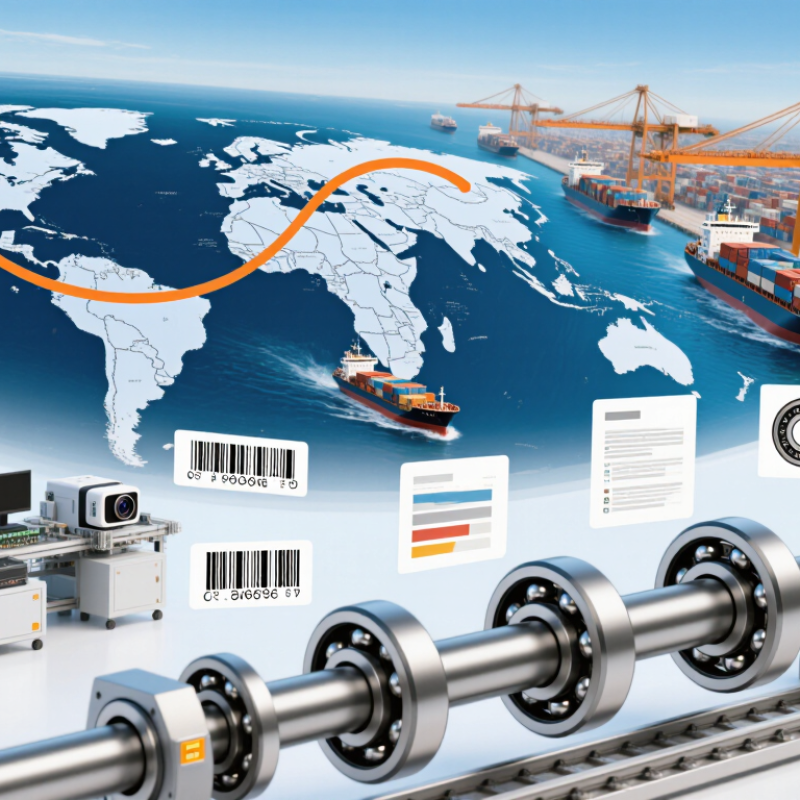
| 8. Packaging | Protection during international transport | Prevent corrosion, impact, contamination, and rail deformation during handling and long-distance transport. | Each unit should be sealed or protected with suitable rust-prevention material, immobilized, labelled, and packed with shock protection. | Export cartons, reusable cases, moisture indicators, desiccant, barcode labels, and custom pallet dimensions may be specified. | Perform packaging inspection, carton-weight verification, label review, and, for sensitive shipments, vibration or drop-risk assessment. | State carton dimensions, gross weight, pallet requirements, marking language, and wood-packaging compliance requirements. |
| 9. Delivery Terms | Lead time and Incoterms | Separate sample lead time, production lead time, inspection time, and transit time in the quotation. | Illustrative planning target: samples in 2–4 weeks; standard production in 4–8 weeks after drawing approval and deposit. | Custom tooling, special materials, or low-volume production may add engineering and manufacturing time. | Track production milestones, inspection release, booking confirmation, commercial invoice, packing list, and transport documents. | Compare FCA, FOB, CPT, CIP, or DAP under Incoterms® 2020; clearly define exporter, importer, insurance, and customs responsibilities. |
| 10. Final Supplier Decision | Total landed cost and risk | Evaluate unit price together with tooling, inspection, freight, duties, warranty, replacement cost, and delivery reliability. | Approve only samples that meet dimensional, functional, documentation, and packaging requirements without unresolved deviations. | Document all approved deviations, engineering changes, minimum order quantities, and future volume-price conditions. | Use a weighted scorecard: technical compliance 35%, quality system 20%, delivery 20%, total cost 15%, communication 10%. | Sign a quality agreement covering warranty period, replacement procedure, corrective-action response time, records, and audit rights. |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS