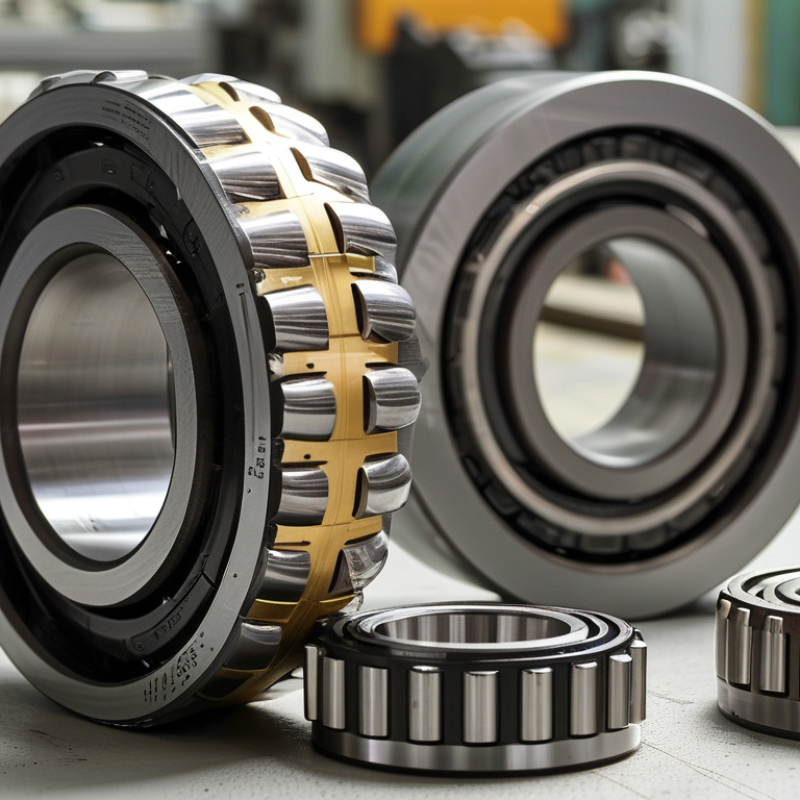
| Part-number identification | HB88509 is a part-number reference for a center support bearing assembly. The part number alone should not be treated as a complete dimensional specification. | Request a dimensional drawing, application list, shaft configuration, and vehicle identification information. Compare the supplied data with the original service requirement. | All critical dimensions and application references must be documented before quotation or sampling. | 10% |
| Critical dimensions | - Bearing inner diameter
- Outer diameter
- Overall bearing width
- Mounting-hole spacing
- Support-bracket height
- Flange or shaft interface dimensions
| Check the drawing with calibrated vernier calipers, micrometers, bore gauges, and a dedicated checking fixture where required. | Every dimension must match the approved drawing tolerance. Do not accept a part based only on a visual similarity or part-number label. | 15% |
| Bearing tolerance and running accuracy | Radial bearing tolerances should be stated according to the applicable bearing standard. ISO 492 provides tolerance classifications for rolling bearings. | Review the inspection report for bore, outside diameter, radial runout, and rotational smoothness. Confirm the stated tolerance class and measurement method. | Inspection results must be traceable to calibrated equipment and remain within the approved drawing and tolerance class. | 10% |
| Bearing internal construction | Confirm bearing type, row arrangement, cage material, seal arrangement, internal clearance, and grease specification. | Review the technical data sheet and, when necessary, conduct a sample teardown or laboratory inspection. | The construction, seal arrangement, internal clearance, and lubricant must be consistent across the approved production sample and mass-production parts. | 8% |
| Rubber support quality | Important properties include rubber compound, hardness, bonding condition, resistance to cracking, and resistance to oil, ozone, and temperature exposure. | Request rubber material information, hardness results, bonding inspection, and test data for heat aging and ozone resistance where applicable. | Rubber hardness and material requirements must be defined on the approved specification. No visible cracks, separation, swelling, or incomplete bonding are acceptable. | 12% |
| Dynamic balance and vibration control | Center support bearing assemblies influence propeller-shaft alignment and vibration. Dynamic balance requirements depend on the shaft assembly and vehicle application. | Ask for the balancing grade or maximum residual unbalance requirement, balancing speed, test method, and test records. | The supplier must provide a written balance requirement and repeatable test records for each approved production configuration. | 10% |
| Load and durability capability | Evaluation should consider radial load, axial load, rotational speed, temperature, grease life, and expected operating cycle. | Review engineering calculations, endurance-test conditions, test duration, failure criteria, and final inspection records. | Test conditions must represent the intended service environment, and the report must identify sample quantity, test duration, and measured results. | 12% |
| Material traceability | Traceability should cover bearing steel, rubber compound, bracket material, seals, grease, and production batch. | Check heat numbers, incoming inspection records, batch codes, production dates, and final inspection links. | Each shipment should be traceable to a production batch and corresponding inspection documentation. | 8% |
| Quality-management system | A documented quality system should control design changes, nonconforming products, corrective actions, calibration, and process inspection. | Review valid quality-system certificates, audit summaries, process-control plans, and corrective-action records. | Certificates must be valid, applicable to the manufacturing site, and supported by actual process records. | 7% |
| Sample consistency | Production samples should match the approved sample in dimensions, materials, marking, packaging, and performance. | Compare pre-production, pilot, and mass-production samples using the same inspection checklist. | No uncontrolled change is acceptable. Any change to material, tooling, process, or design should require written approval. | 5% |
| Inspection and documentation | Required documents may include a dimensional report, material certificate, rubber test report, balance report, endurance report, and certificate of conformity. | Check document revision, test date, batch number, inspector, equipment identification, and approval status. | Documents must be complete, consistent with the shipped batch, and available in English or an agreed technical language. | 6% |
| Packaging and storage | Packaging should protect the bearing from moisture, contamination, impact, deformation, and long-term storage damage. | Inspect internal protection, carton strength, batch labels, storage instructions, and transport test results where applicable. | Parts must arrive clean, dry, undamaged, correctly identified, and suitable for the agreed storage period. | 4% |
| Commercial and after-sales control | Evaluate lead time, minimum order quantity, sample policy, warranty period, replacement procedure, and response time for quality claims. | Request written commercial terms and review the supplier's documented complaint-handling process. | Terms must be written clearly, including warranty scope, evidence requirements, corrective-action timing, and replacement responsibility. | 3% |
| Final supplier decision | Use a weighted score based on technical compliance, quality evidence, sample performance, traceability, and commercial reliability. | Score each dimension from 0 to 100, multiply by the assigned weight, and retain all supporting documents. | A supplier should not be approved if any safety-critical dimension fails, even when the total score is high. A practical approval target is at least 80/100 after all critical items pass. | 100% |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS