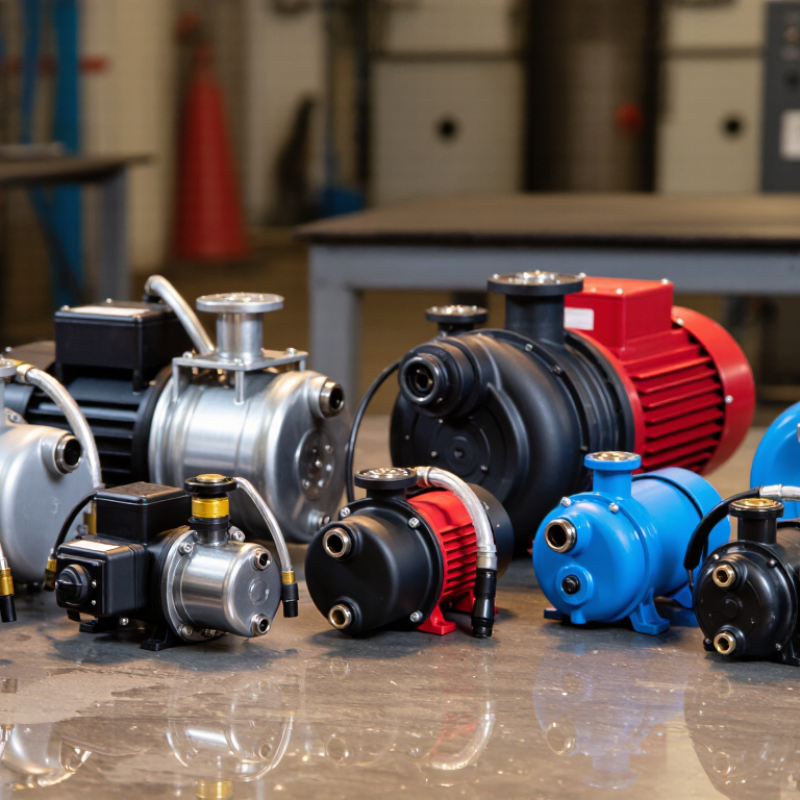
| 1 | Oil-Sealed Rotary Vane Pump | 1 × 10⁻³ to 5 × 10⁻² mbar | Atmospheric pressure to high vacuum | 1–100 m3/h | Positive-displacement compression using rotating vanes and lubricating oil | Strong starting performance, high water-vapor tolerance with gas ballast, broad availability, and competitive cost | Oil backstreaming can contaminate the vacuum system; requires oil maintenance and exhaust filtration | Vacuum packaging, freeze-drying support, metallurgy, laboratory systems, and general industrial evacuation |
| 2 | Dry Screw Pump | 1 × 10⁻² to 1 × 10⁻³ mbar | Atmospheric pressure to medium/high vacuum | 10–500 m3/h | Non-contact screw rotors transport and compress gas without process oil in the pumping chamber | Clean, oil-free vacuum, good chemical resistance, high throughput, and suitability for continuous industrial duty | Higher purchase price; may require purge gas, inlet filtration, and protection against condensable or abrasive loads | Semiconductor processing, chemical drying, coating, battery production, and centralized vacuum systems |
| 3 | Scroll Pump | Approximately 1 × 10⁻² to 1 × 10⁻³ mbar | Atmospheric pressure to high vacuum | 1–30 m3/h | Orbiting scrolls reduce the gas volume progressively without lubricating oil in the pumping chamber | Clean dry vacuum, low vibration, relatively quiet operation, and compact installation | Tip seals are wear components; liquid slugs, heavy dust, and large condensable loads can reduce service life | Analytical instruments, electron microscopy, laboratory vacuum, medical equipment, and clean research systems |
| 4 | Diaphragm Pump | Approximately 1–5 mbar | Atmospheric pressure to rough vacuum | 0.5–15 m3/h | Flexible diaphragms alternately expand and compress chambers with check valves controlling gas flow | Oil-free operation, good chemical compatibility with suitable diaphragm materials, simple maintenance, and low operating cost | Cannot normally reach high-vacuum pressures; diaphragm and valve materials limit temperature and solvent compatibility | Filtration, rotary evaporation, vacuum concentration, gas sampling, and backing smaller high-vacuum pumps |
| 5 | Roots Booster | Down to approximately 1 × 10⁻³ to 1 × 10⁻⁵ mbar with a backing pump | Typically used from rough/medium vacuum into high-vacuum systems | 100–5,000 m3/h | Two synchronized lobed rotors transfer gas at high volume without internal contact | Very high volume flow, faster pump-down, oil-free compression chamber, and strong performance at medium vacuum | Requires a backing pump; direct operation at atmospheric pressure is limited unless equipped with bypass or variable-speed control | Large vacuum chambers, vacuum furnaces, freeze-drying, coating lines, and industrial evacuation systems |
| 6 | Turbomolecular Pump | Approximately 1 × 10⁻⁷ to 1 × 10⁻⁹ mbar | High vacuum to ultra-high vacuum | 50–2,000 L/s for nitrogen, depending on model | High-speed angled rotor and stator blades transfer momentum to gas molecules | Clean high vacuum, rapid removal of light gases, low hydrocarbon backstreaming, and precise vacuum control | Needs a backing pump; sensitive to particulates, sudden venting, vibration, and excessive foreline pressure | Surface analysis, semiconductor equipment, mass spectrometry, electron microscopy, and research vacuum chambers |
| 7 | Diffusion Pump | Approximately 1 × 10⁻⁷ to 1 × 10⁻⁹ mbar | High vacuum to ultra-high vacuum | 100–10,000 L/s for nitrogen, depending on pump size | High-speed vapor jets entrain gas molecules and direct them toward a cooled pump wall and backing pump | High pumping speed, robust construction, good tolerance for continuous high-vacuum operation, and attractive cost per unit of pumping speed | Requires heater power and cooling; possible vapor backstreaming; needs a backing pump and suitable baffles or traps for clean processes | Vacuum coating, metallizing, vacuum furnaces, large research systems, and high-throughput industrial chambers |


 08045479132
 Send Inquiry


 Send Inquiry
 Send SMS