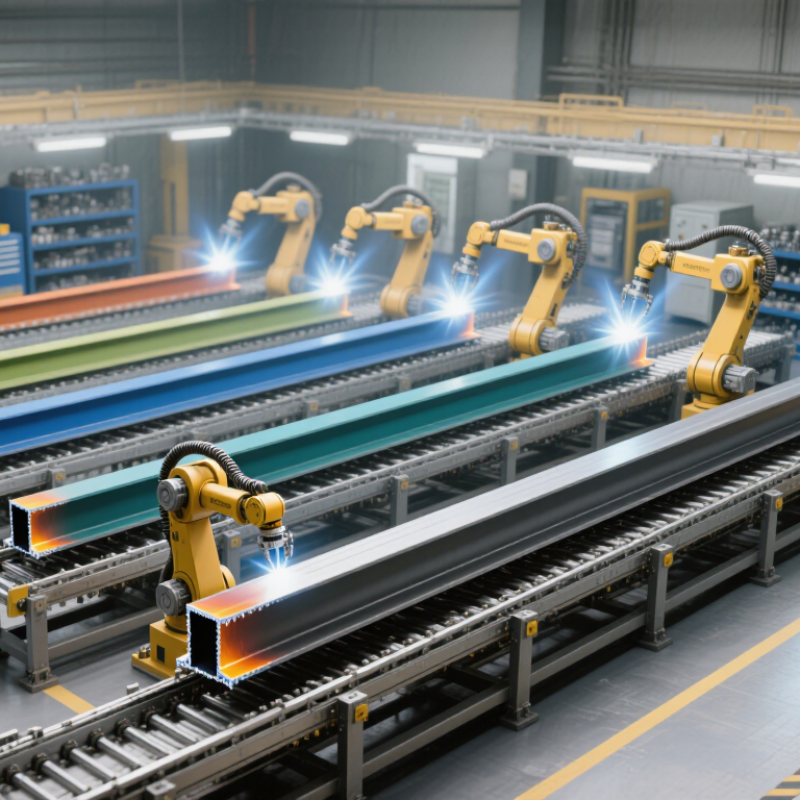
| 1. Standard Submerged Arc Welding (SAW) Line | Mechanized SAW heads weld the longitudinal web-to-flange fillets while the beam is held in alignment. | General structural fabrication and recurring T-beam production. | SAW is well suited to long, continuous welds and can provide high deposition rates with consistent operating conditions. | Confirm the specified joint geometry, welding positions, flux handling, seam tracking method, and supported steel thickness range. |
| 2. Twin-Head Simultaneous Welding Line | Two welding heads work on opposing longitudinal seams at the same time, where the machine design and weld sequence allow. | Shops seeking shorter cycle times on repeatable beam sizes. | Simultaneous welding can reduce the time spent on the two main seams and help balance heat input across the section. | Check head spacing and adjustment range, access to both seams, distortion-control procedure, and whether both sides can be welded for every specified section. |
| 3. Single-Head Adjustable Line | One mechanized welding head is repositioned or the workpiece is reoriented to complete the required seams. | Low-to-medium production volumes and workshops making varied T-beam sizes. | Typically offers a simpler layout and greater flexibility for changing beam dimensions or production schedules. | Ask how much changeover is required between sizes, how the beam is turned or indexed, and whether the operating sequence meets the required output. |
| 4. Heavy-Section T-Beam Line | Heavy-duty fixtures, supports, and welding equipment are configured for larger or heavier structural sections. | Fabricators handling thick plates, long beams, or high workpiece loads. | Designed around workpiece support, clamping, and handling needs that can exceed the capacity of a light-duty line. | Verify maximum workpiece weight and length, plate-thickness limits, fixture capacity, crane or roller-table requirements, and foundation details. |
| 5. Compact Workshop Line | A space-conscious arrangement combines beam positioning and mechanized welding within a smaller production footprint. | Smaller fabrication facilities or operations with limited floor space. | Can simplify installation and material flow where a large, fully integrated line is not practical. | Measure the complete operating envelope, including loading, unloading, maintenance access, fume extraction, and safe movement of long workpieces. |
| 6. CNC or Servo-Controlled Flexible Line | Programmed axes or servo adjustments set welding-head position and, depending on the machine, support repeatable setup changes. | Production involving multiple section sizes or frequent repeat orders. | Stored settings and controlled positioning can help make changeovers more repeatable than manual adjustment alone. | Request a live demonstration of a size change, confirm supported adjustment axes, check program storage and operator training, and clarify which settings remain manual. |
| 7. Integrated Material-Handling Line | Welding equipment is combined with infeed, positioning, conveying, and outfeed equipment; the exact level of automation varies. | Higher-throughput production with a consistent product mix and planned material flow. | Integration can reduce manual transfers between operations and coordinate welding with workpiece handling. | Review line layout, interface responsibilities, safety interlocks, handling capacity, maintenance access, and the effect of bottlenecks on total cycle time. |


 08045479132
 Send Inquiry

 Send Inquiry
 Send SMS